 English
 русский
Plastic injection mold runner system design points

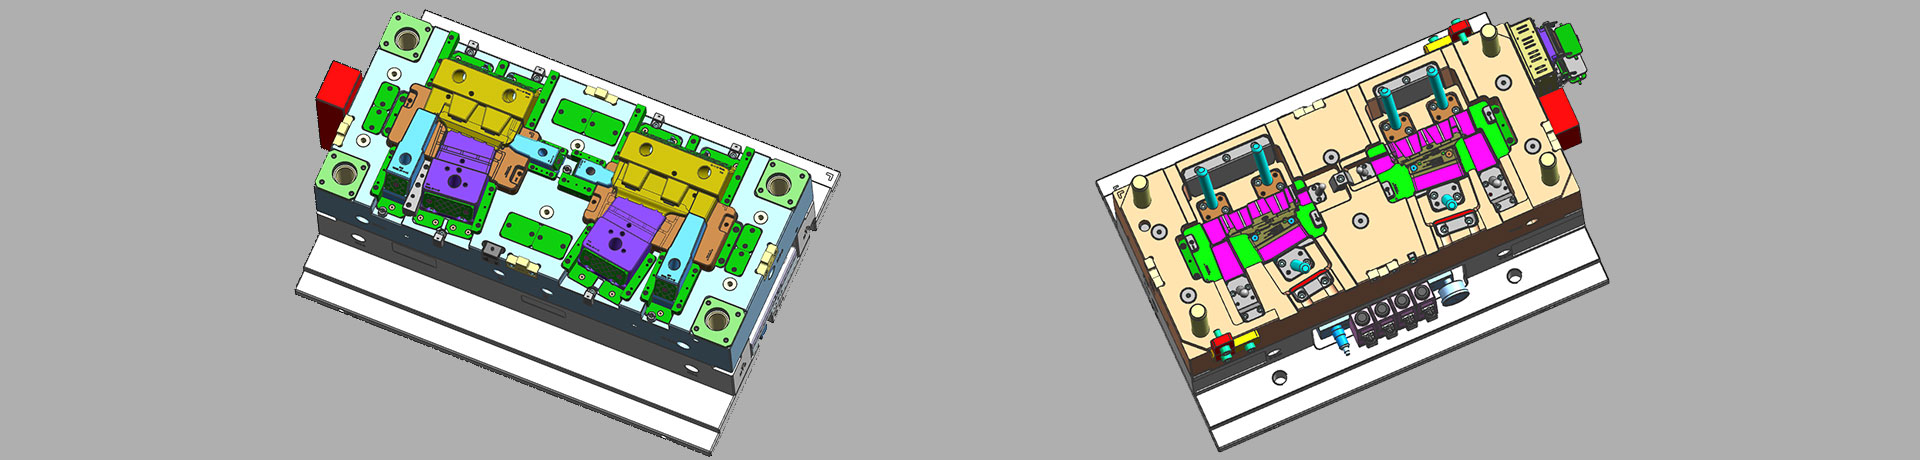
When designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically considered to minimize the proportion of waste generated by the runner; finally, it should be easy to repair the gate mark on the plastic part.
The main points of gating system design are as follows:
1. The gate positio should ensure that when the plastic flows into the cavity, it faces the wide part of the cavity, that is, the melt should flow from the thick-walled part of the cavity into the thin-walled part. If the melt flows from the thin-walled part to the thick-walled part, the speed will drop quickly and the temperature will drop rapidly which is not conducive to filling;
2. In order to prevent the plastic rushing to the cavity, core or insert directly, it is necessary to ensure that the plastic melt can flow to all parts of the cavity as soon as possible and to avoid deformation of the core or insert;
3. Try to avoid making plastic parts cause weld marks, and make the weld marks occur in unimportant parts;
4. The gate position and its plastic inflow direction can flow in evenly along the parallel direction of the cavity when the plastic flows into the cavity, and it is conducive to the discharge of gas in the cavity;
5. If fully automatic operation is used during production, it must be ensured that the condensate of the gating system can be smoothly and automatically demolding together with the plastic parts;
6. There should be a good venting structure and sufficient cold well in the gating system, the air and cold material in the gating system should be brought into the cavity as less as possible, which will affect the parts quality;
7. When a mold has multiple cavities, it is necessary to prevent the plastic parts with very different sizes from being placed in the same mold, if the part size differs by more than 4 times, it is difficult to make filling balanced;
8. If the projected area of the plastic part is big, we should avoid opening a gate on one side of the mold when designing the gating system, otherwise it will cause uneven force during injection molding;
9. The design of gating system should consider shortening the production cycle and increasing productivity.


Design Tips of Vacuum Venting Mold
Mar 30, 2022There are some regular venting way which are parting surface venting, insert venting, insert pin venting and well-ventilated steel, but there is a special way is vacumm venting, it will need vacumm...view
Different treatment of plastic injection mold cooling system principles
Feb 22, 2022Different treatment principle: 1. The mold temperature is different according to the different plastics, when the plastic requires the molding temperature of the mold to be ≥80°C, the mold must be...view
Hydraulic diameter conversion of runners in plastic mold gating system design
Jan 13, 2022Hydraulic diameter refers to 4 times the ratio of the flow cross-sectional area to the perimeter, as the wall shear stress of non-circular pipes is not even distributed along the surrounding walls,...view
Key points of plastic injection mold runner system
Jan 12, 2022The sub-runner is a transitional channel between the main runner and the gate, as the sub-runner is the longgest part of gating system, so it is very important to enhance the parts quality and improve...view
What is Plastic Injection Mold?
Dec 27, 2021The plastic mold is used for injection molding, it is assembled with cavity, core and side slider together, with ejection system and adjustments to produce plastic products by different shapes and...view
Limitations of gas-assisted injection molding technology
Apr 25, 2022Gas-assisted injection molding technology has obvious advantages in thick wall thickness and pipe parts, but this technology still has many limitations, which are mainly reflected in the following...view